Conveyor belts
The machinery
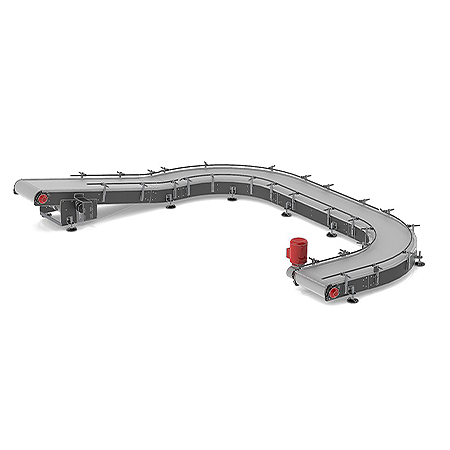
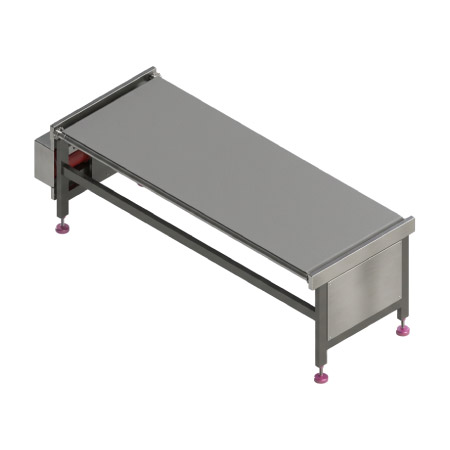
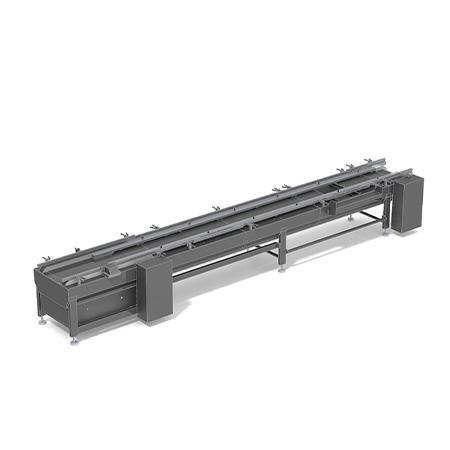
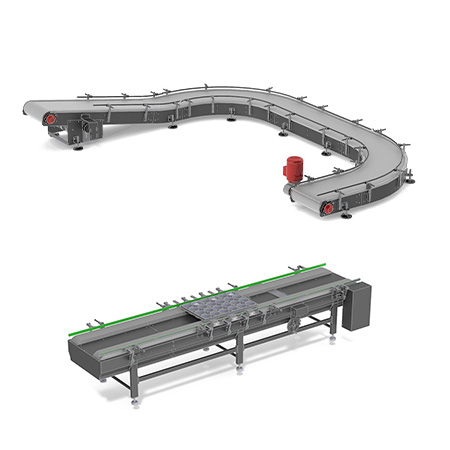
One of the most common challenges in food production facilities is the proper handling of products. This need can be addressed through conveyor systems custom-designed for different types of facilities and the items to be handled. Our line of conveyor belts includes a wide range of solutions. The variety of materials available for the structures allows us to meet every need, from industrial packaging to the most stringent food-grade environments. Thanks to our experience, we also manufacture small rotary conveyor lines and dedicated conveyor stations for every type of product. All our conveyors comply with current regulations and meet the mechanical specifications requested by the customer, making customization their main strength. The use of state-of-the-art mechanical and electronic components also enables us to meet the most complex requirements.
Translated with DeepL.com (free version)
Key Features
- Low maintenance
- High operational flexibility
- Easy to use
- Quick to clean
Areas of application
Bellini Machines’ conveyor belts are used in a wide range of manufacturing sectors, adapting easily to different types of containers and processes. Thanks to their flexibility, they ensure rapid integration into existing production lines and provide effective support for packaging and handling operations.
Bakery
Food
Beverage
Packaging
Cosmetics
Pharmaceuticals
Pet food
Request further information
Please fill in the contact form; a member of our team will get in touch with you as soon as possible.
The machinery
In this section, you’ll find answers to frequently asked questions to help you better understand how our machinery works and the services we offer. Quick and clear support to guide you in choosing and using our solutions.
What types of conveyor belts does Bellini Machines manufacture?
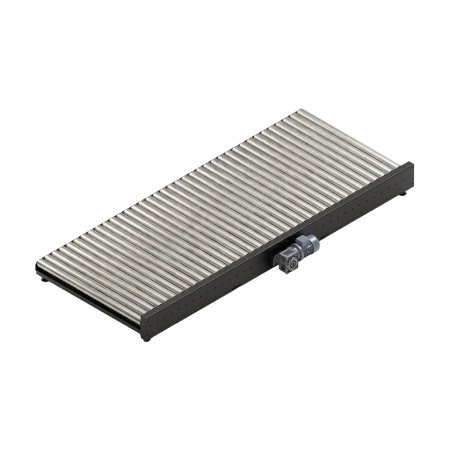
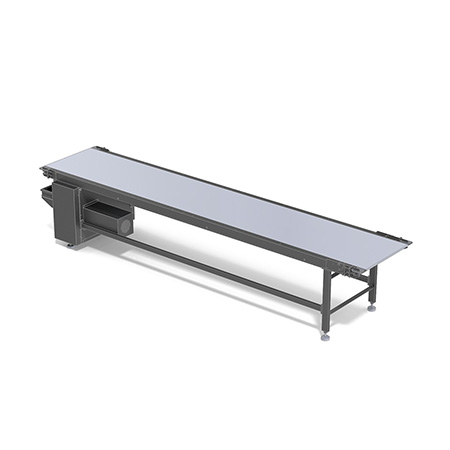
Bellini Machines manufactures modular plastic-mesh or tabletop chain conveyors, slat conveyors, wire mesh conveyors, belt conveyors, and motorized roller conveyors. The product line meets every need, from industrial packaging to the most stringent food-grade environments that require complete sanitizability.
How do you choose the conveyor belt model that best suits your application?
The choice depends on several factors: the type and weight of the product being transported, the required line speed, the industry’s hygiene requirements, the operating temperature, and the need for curves or elevation changes. For each application, Bellini Machines designs a custom conveyor belt that is best suited to the application, ensuring compliance with the customer’s mechanical specifications and regulatory requirements.
Can Bellini Machines conveyor belts come into direct contact with food?
Yes. The belts are designed in accordance with current regulations governing food contact. The materials used for the load-bearing surfaces—food-grade plastic, stainless steel, and wire mesh—are selected to comply with EU directives on materials intended to come into contact with food.
Is it possible to build small rotary lines using Bellini Machines belts?
Yes. Thanks to its experience in the industry, Bellini Machines also manufactures small rotary molding lines and conveyor stations designed for all types of products. These compact solutions are ideal for completing the production cycle without having to rely on external components.
Can conveyor belts be customized to meet the specifications of the production line?
Yes, customization is the main strength of Bellini Machines conveyors. Each conveyor is custom-designed and manufactured to meet the customer’s specific mechanical requirements: length, width, conveyor height, incline, type of conveyor surface, and drive system.
How do you clean a conveyor belt in a food-processing environment?
Bellini Machines conveyors are designed for immediate cleaning. Depending on the model, they can be washed with water, cleaned using approved food-grade detergents, and the support surface can be quickly disassembled. The modular plastic-mesh conveyors allow for the partial replacement of modules without shutting down the entire line.
What is the difference between a conveyor belt and a table-top modular chain conveyor?
The carrier belt uses rigid crossbars that support products even on inclined paths, making it ideal for handling unstable objects or those being transported uphill. The modular table-top chain conveyor offers a continuous, smooth surface, suitable for products that require lateral movement, accumulation, or transfer between lines.
Can conveyor belts be integrated with advanced control systems?
Yes. The use of state-of-the-art mechanical and electronic components allows us to meet even the most complex requirements: speed encoders, presence sensors, variable-speed drives, and integration with Siemens, Omron, Allen-Bradley, and Schneider Electric PLCs via PROFINET, EtherCAT, EtherNet/IP, and CANopen protocols.
In which industrial sectors are Bellini Machines conveyor belts used?
Bellini Machines conveyor belts are used in the bakery, food, beverage, packaging, cosmetics, pharmaceutical, and pet food industries. Their flexible design allows them to be used in both dry packaging environments and humid environments in the food and dairy industries.